Custom CZ Purlin Roll Forming Machine Company for Reliable Steel Framing Solutions
2026-10-29
In steel framing, the difference between a project that runs smoothly and one plagued by delays often comes down to the equipment behind it. Custom CZ purlin roll forming machines are the backbone of reliable structural work, but not all manufacturers approach them with the same precision. If you've been searching for a solution that adapts to your exact profiles rather than forcing you into standard specs, it's time to meet Beenew. Here's what sets their approach apart.
How Interchangeable CZ Profiles Trim Setup Downtime
Swapping out a worn or damaged CZ profile used to mean pulling maintenance off other tasks for hours. With interchangeable profiles, the replacement slides into the same mounting points, uses the same fasteners, and lines up without re-drilling or shimming. Because the cross-section and slot spacing are consistent across batches, you don't have to measure twice or file down edges just to get a clean fit.
Setup changes on assembly lines often stall when a custom-cut extrusion doesn't match the existing frame. Interchangeable CZ profiles remove that bottleneck. Operators can unbolt one segment, drop in a different length or angle, and tighten it down. The pre-machined holes and T-slot geometry mean the new piece aligns with the surrounding structure immediately.
This also helps during product changeovers. Instead of building new jigs or guards from raw stock, teams keep a small inventory of standard CZ profiles and connectors. A guard rail that needs to be three inches shorter is simply swapped for a shorter profile; no cutting station, no waiting for a machinist, no extended line shutdown.
Designing Roll Sets Around Your Toughest Steel Specs
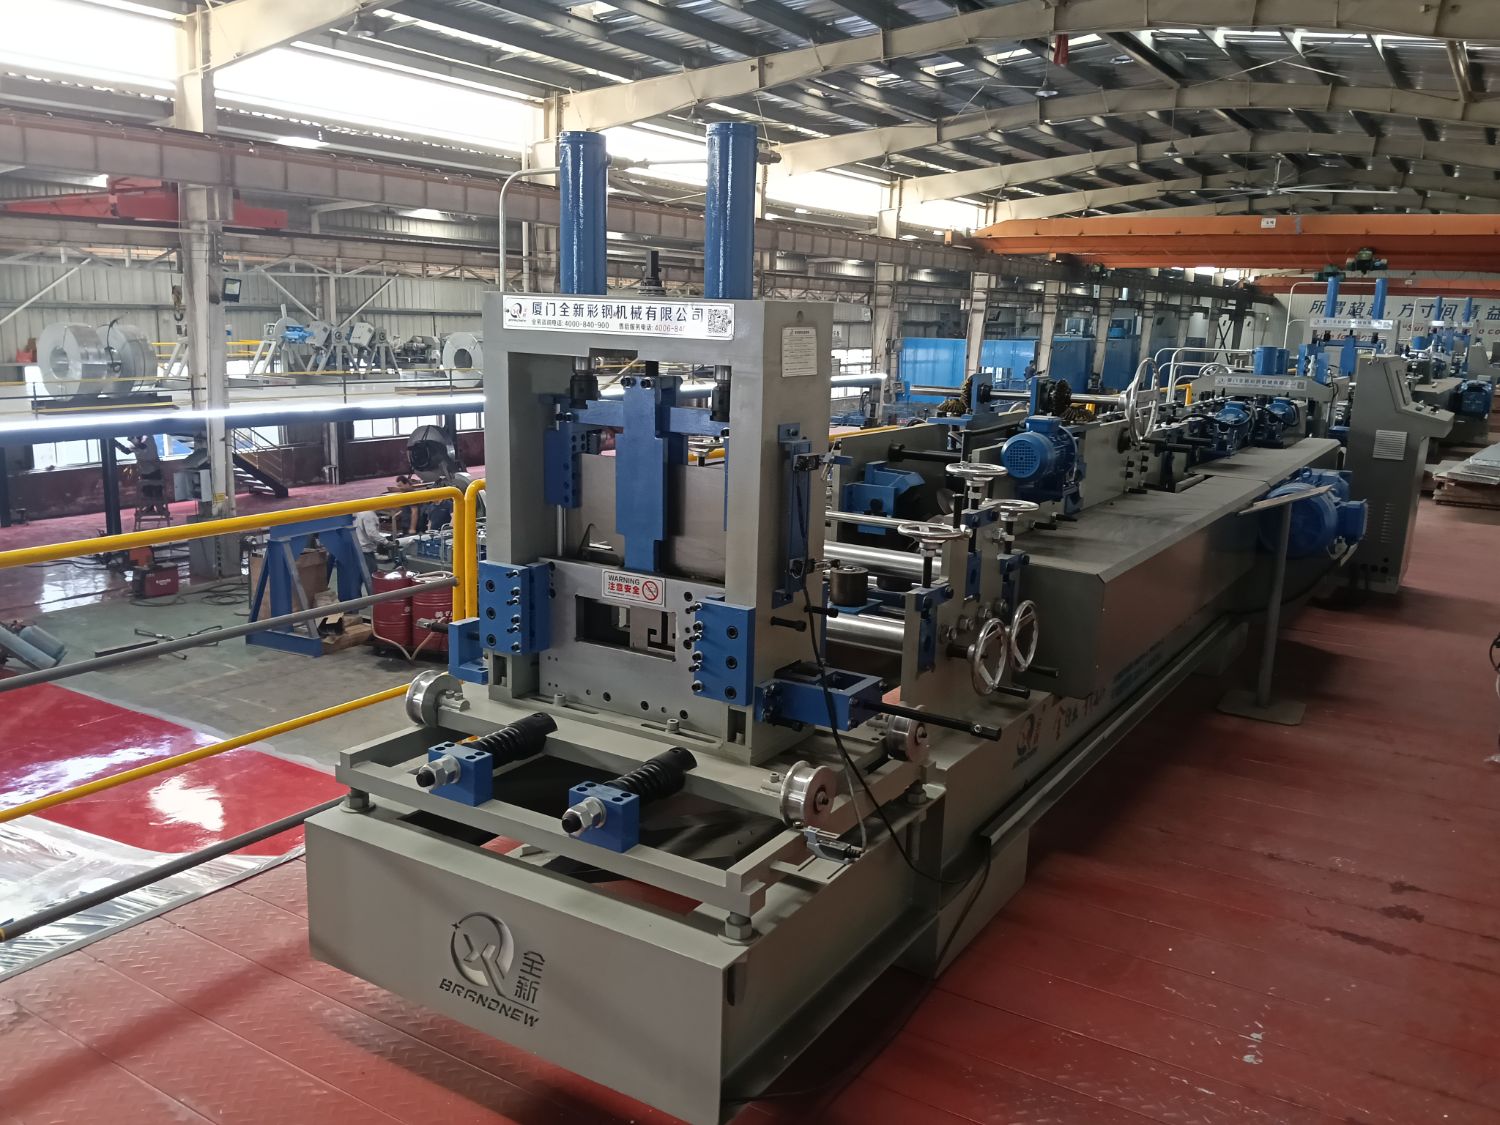
When steel gets harder to form, the usual roll set geometry stops being forgiving. Instead of copying proven profiles from mild stock, we start by mapping the exact yield-to-tensile spread, springback angle, and edge condition of the specific heat or coil. Those numbers dictate how much overbending each pass needs, whether the roll gap must widen, and where to add side roll pressure before the strip thinks about twisting. Small adjustments here prevent the downstream headaches that show up as camber, edge wave, or split corners.
The most punishing specs often demand a split in responsibility between driven and idle passes. We might design the first few stands to do aggressive work while the steel still has some ductility left, then let later stands act as stabilizers rather than shapers. For ultra-high-strength material, that means fewer forming passes, not more, and roll materials that can shrug off surface stress without picking up pickup. The tooling itself gets treated as a wear surface, not a fixed shape.
A roll set built this way usually needs to be proven on one coil before we trust it with a full run. We dial in the final profile using measured strip shape from the exit end, not just CAD prediction. The goal is a roll set that holds the tightest dimension on the toughest spec without requiring constant operator correction.
Why Coil Feed Consistency Shapes Every Purlin
On a roll forming line, the steel strip never really stops moving. Any tiny hesitation or surge in the coil feed gets carried straight into the profile being formed, and by the time the strip reaches the final pass, those variations show up as inconsistent web depths, flange widths, or lip angles. It is rare for a single feed fluctuation to be obvious, but over hundreds of purlins the cumulative effect means parts that look close enough yet behave differently under load.
Hole placement is where feed inconsistency becomes impossible to ignore. Most purlins are pre-punched for bolted connections, and the encoder tracking strip length relies on a steady, repeatable feed rate. If the coil slips or the tension between the decoiler and the forming mill drifts, the measured length no longer matches the actual material position. Bolt holes end up shifted by a few millimeters, which might not sound like much until an installer has to enlarge every fourth hole on a roof run. Closed-loop servo feeds help, but they cannot fully compensate for a feed path that is not mechanically stable.
Perhaps the most overlooked effect is residual stress. When feed speed varies, each bend forms under slightly different strain conditions, leaving uneven stress locked into the purlin. Over time, or under temperature changes, these stresses release as side bow or twist, which then transfers to the roof or wall system. A purlin that leaves the mill looking straight can develop a visible sweep weeks later. Consistent feeding keeps the forming process in a narrow window, giving every purlin the same internal state, not just the same outer dimensions.
The Overlooked Role of Straightening in Framing Quality
Most people spend hours agonizing over mat colors, frame profiles, and glass types, yet the single most common flaw I see in finished pieces is a barely perceptible tilt. A photograph or print that’s off by less than half a degree won’t jump out at first glance, but it creates a low-grade visual discomfort that viewers can’t quite name. They might say the piece feels “off” or “unsettled,” and more often than not, the culprit is a horizon line or subject edge that wasn’t properly straightened before mounting.
Straightening isn’t just about aligning the image within its borders — it’s also about how the paper or canvas sits inside the frame. If the substrate itself is slightly skewed, even a perfectly leveled image will look wrong because the margins become unequal. This is especially noticeable on wide mats, where a two-millimeter drift can make the whole presentation feel haphazard. I’ve learned to check alignment with a long metal ruler against the frame rebate, not just by eye, because our brains are surprisingly good at ignoring tiny errors until they accumulate into something obvious.
One trick that rarely gets mentioned is to straighten the work before you even pick up the frame. Lay the print on a flat surface, align it with a grid cutting mat, and use removable tape to anchor the corners without tension. Then, when you place it into the frame, re-check with a small bubble level held against the top edge of the glass. The difference between a piece that’s “nearly straight” and one that’s truly plumb and level is subtle, but it’s the kind of detail that separates a rushed job from a professional finish.
Tailored Punching Patterns Without Slowing the Line
Custom hole patterns used to mean either accepting a generic layout or losing precious seconds to manual changeovers. The problem isn't the punching itself—it's the pause that comes with reconfiguring tooling between jobs. Modern lines solve this by embedding programmable punch heads that shift between pattern presets on the fly, so a single coil can feed dozens of different hole geometries without a single stop.
What makes this practical at full speed is the use of servo-driven rams paired with real-time pattern sequencing. Instead of physically swapping dies, the control system adjusts stroke position, spacing, and punch selection between cycles. A job that once required a ten-minute setup now happens during the natural rhythm of the line, with the controller reading barcode or RFID data from each incoming blank and applying the matching punch recipe milliseconds later.
The result is a line that handles mixed orders back-to-back while keeping throughput steady. Operators stop worrying about batching similar parts to avoid slowdowns, and downstream assembly gets exactly the hole layout each unit needs. The flexibility doesn't come from running slower—it comes from making the changeover invisible.
What a Support Partner Should Bring After Commissioning
Once the system goes live, the real test of a support partner begins. They should arrive with more than just a phone number — a clear escalation path, named contacts who understand the installation, and a realistic response-time commitment that matches your operational hours. If a critical failure happens at 2 a.m., you don’t want to be routed through three generic call centers before reaching someone who even knows your site layout.
Beyond break-fix, a solid partner brings proactive monitoring and a schedule for routine health checks. That means firmware updates, log reviews, and performance tuning done on a predictable cadence — not just reacting when things break. You should also get access to training materials or refresher sessions for your own team, so small issues get resolved in-house instead of waiting on a ticket.
Finally, look for someone who documents what they did during commissioning and hands over a clean handoff package: as-built drawings, configuration files, spare parts lists, and a warranty summary that spells out exactly what’s covered. If they leave you digging through emails for a password or a manual, that’s a red flag. The best partners make you feel like you’re not the only one responsible for keeping the system healthy.
FAQ
Yes. We don't force you into a fixed size range. Our engineering team works from your drawings or a sample profile and adjusts roll stations, shaft centers, and punch positions to match. Typical custom depths range from 80 mm to 350 mm, but we can go further if your framing system needs it.
Most of our CZ lines are designed for 1.5 mm to 3.5 mm galvanized or cold-rolled steel. If you need to run 4.0 mm high-strength coil, we can upgrade the drive train and add pre-straightening. We'll ask about your common coil specs before finalizing the design.
Yes. A single line can produce both C and Z sections by switching the roll setup or using a quick-change cassette system. The changeover usually takes 20 to 40 minutes depending on the automation level, so you won't need two separate machines for residential or light commercial framing.
We use servo-driven punching units synced with the flying shear. The controller reads the target length and hole positions from your cutting list, then fires the punches before the cut. This avoids accumulated errors and lets you run mixed purlin lengths in one batch without manual stops.
Absolutely. The machine is built for both structural framing and cladding support. You can run C sections for wall girts and Z sections for roof purlins. The adjustable flange width and lip size also help match the load tables your engineer specifies.
We send a commissioning engineer to your factory for mechanical setup, PLC tuning, and operator training. After that, you have remote video support and spare parts shipped by air or sea. Most wear parts like rollers and punch dies have a clear replacement schedule, so downtime stays predictable.
We pay close attention to roll pass design and use hardened, polished rollers with surface treatments where needed. Guiding rollers and straightener rolls have adjustable pressure, so prepainted and galvanized coils keep their coating. We also include coil edge guides to prevent scraping on the entry side.
A standard custom line usually leaves our workshop within 45 to 60 working days after drawing approval. If you need a faster schedule, we can split production and pre-assemble the electrical panels while the roll stands are being machined. Shipping time depends on your port, but we handle export packaging and container loading.
Conclusion
A custom CZ purlin roll forming machine earns its keep long before the first purlin exits the line. The ability to switch between C and Z profiles without a drawn-out retooling session changes how a shop schedules production. Instead of losing hours to setup, operators can move from one profile to the next in minutes, which matters more when steel specs vary widely from job to job. Designing roll sets around the toughest material you actually run—not a generic baseline—means the machine holds dimensional accuracy even when the coil gauge, yield strength, or coating pushes the limits. Feed consistency is another quiet factor: if the coil doesn't enter the forming stands at a steady, controlled pace, every downstream station inherits that error. A well-matched decoiler and leveler loop keeps the strip tension predictable, so each purlin comes out with the same web, flange, and lip dimensions.
Straightening is often treated as an afterthought, yet it has a direct bearing on framing quality. A purlin that carries a slight camber or twist from the mill will create headaches for erectors trying to align roof and wall framing. Purpose-built straightening heads, tuned to the profiles you produce, remove that residual stress before cutoff. Tailored punching patterns are another area where a custom approach pays off. Whether you need slots, holes, or access cutouts at non-standard spacings, the right punch tooling and control logic let you add those features inline without slowing the forming speed. Finally, the relationship shouldn't end at commissioning. A dependable supplier brings more than a manual—they offer responsive troubleshooting, spare roll and punch components, and production advice when you take on an unfamiliar steel grade or profile. That kind of support keeps the line running reliably year after year, which is ultimately what steel framing contractors need.
Contact Us
Contact Person: Sophie
Email: [email protected]
Tel/WhatsApp: 8615959271231
Website: https://www.beenew-rollformer.com/