Filling and Sealing Machine Exporter Insights for Smarter Packaging Decisions
2026-11-16
Packaging lines rarely get the attention they deserve until a filling or sealing issue slows everything down. For buyers comparing equipment across markets, the difference between a smooth launch and a costly retrofit often comes down to the exporter’s engineering depth and after-sales response. This guide pulls practical insights from real filling and sealing machine export projects, with field notes from Wanying Machinery that show where smart packaging decisions actually begin.
Questions Most Buyers Forget to Ask an Exporter
Most buyers focus on unit price, lead time, and payment terms, then call it a day. The problems usually show up later in the details nobody thought to put in writing. Things like who is responsible for demurrage if the container sits at the port over a holiday, what the actual tolerance is on the product dimensions, or whether the factory will cover the cost of a third-party inspection when the first shipment fails. A sharp exporter won't wait to be asked, but if they do not bring these up themselves, you should start digging.
Another area that gets skipped is the gap between sample and bulk. A buyer may approve a pre-production sample without asking how much variation to expect once the line is running fast. If the contract does not spell out an acceptable defect rate or says nothing about rework costs, every disagreement becomes a negotiation. Ask what happens when goods are rejected, how long rework actually takes, and who pays for storage while the issue is sorted out.
It also helps to ask for the story behind the factory, not just the trade company in front of you. Request the mill name, recent production lines, and whether you can speak with someone on the floor before the order is placed. If the exporter hesitates on that, treat the hesitation as information.
What Fill Accuracy Claims Leave Out
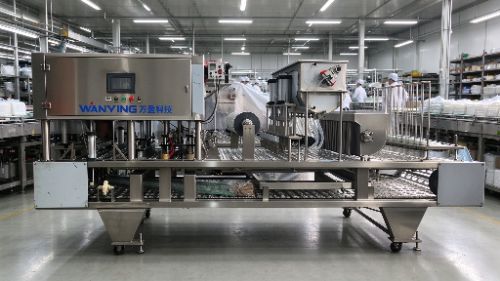
A published fill accuracy figure usually comes from a flat test coupon, a fresh nozzle, and a climate-controlled booth. It will not mention that the same dispensing system drifts when the bead turns a corner or when the paste warms up after twenty minutes of continuous cycling. Those omissions matter because real parts rarely look like the coupon.
Suppliers also tend to report the average, not the spread. If the same setting places 0.4 mm on one part and 0.9 mm on the next, an average of 0.65 mm can still sound respectable. Without the range, the claim hides exactly the inconsistency that causes rework.
Then there is the time factor. A system that holds tolerance for a short demo may walk out of spec after an hour as the seals heat up and the material changes viscosity. Accuracy without a stated duty cycle or recalibration interval is closer to a snapshot than a guarantee.
Sealing Methods That Change More Than Leak Rates
A seal is rarely just a barrier. The choice between a cured-in-place gasket, a compressed fiber sheet, or a metal o-ring shifts how the joint breathes under thermal load, how evenly the flange faces sit at torque, and how much bolt preload survives the first hundred hours. Those secondary effects often show up long before a drip appears.
Installers notice it first as a friction problem. Some coatings and elastomer profiles grip the flange face and turn torque into scatter, leaving the bolts tight but the joint unevenly loaded. Others allow micro-slip that keeps stress from concentrating at the bolt circle. That changes clamp stability, not just the chance of fluid escaping.
Over time, the bigger differences emerge in maintenance and failure mode. A seal that relaxes slowly can hold a flange in place during pressure cycles, while a stiffer material may preserve its shape but transfer more fatigue into the casting. The most interesting choices are not about stopping leaks faster; they are about changing where the system stores and releases strain.
Why Lead Times Vary So Much Between Suppliers
A supplier that stocks common raw materials or semi-finished components can often start production within a few days, while another that orders everything after receiving a purchase order may wait two to six weeks just for materials to arrive. The gap widens further with specialized inputs such as custom alloys, certified plastics, or certain electronic parts, where upstream mills and factories run their own long backlogs.
Production scheduling explains another large part of the difference. A larger workshop with multiple lines can shift capacity around and absorb an urgent order without disrupting existing work, whereas a smaller shop may depend on a handful of skilled operators, so one unexpected job pushes every other order back. Location and freight also matter: an inland supplier relying on multiple trucking legs can easily add five to ten days compared with a supplier near a major port.
Customization and confirmation loops tend to be the least predictable factor. Standard items move quickly because drawings and processes are already fixed, but made-to-order parts often require drawing approvals, sample validation, or back-and-forth on tolerances before production truly begins. Even when the machining or assembly time is short, those waiting periods between revisions can stretch the total lead time by several weeks.
Matching Machine Speed to Real Production Pressure
Running a line at the machine’s advertised top speed rarely translates into steady output. Real production pressure comes from order backlogs, shift targets, and the occasional late supplier, not from a spec sheet. When the equipment is pushed too hard, small hitches turn into long stops: a sensor gets dirty, a roll runs out faster than the crew expects, and quality checks start lagging behind the actual throughput.
The better approach is to match the pace to the constraint that actually governs the shift. On some days that constraint is the curing time, on others it is the operator’s ability to inspect without letting defects slip through. Setting a target speed just under the failure threshold gives the line room to absorb interruptions without collapsing. It also keeps maintenance predictable, because the machine spends less time reacting to jams and more time running in a stable band.
That target should be revisited as orders change. A short run of fragile material may need a slower rhythm, while a large standard order can tolerate a faster pace once the crew has warmed up. The point is not to run slow for its own sake, but to know where the real pressure is and let the machine speed follow that rather than the other way around.
Cost Signals That Surface After Installation
The initial quote rarely tells the whole story. Within the first few weeks, equipment that looked economical on paper often starts revealing its real operating costs through longer cycle times, higher standby draw, or components that wear out faster than the datasheet implied. These are not dramatic failures; they are quiet, repeat expenses that show up on utility bills and maintenance logs, and they tend to be easy to overlook until they have already reshaped the budget.
Some of the clearest signals come from how the system demands attention. A pump that needs recalibration after every power fluctuation, a filter that clogs long before the scheduled replacement, or software that requires paid updates to keep basic functions working are all cost signals, not just annoyances. They indicate that the purchase price was only the entry point, and the real financial commitment is being defined by the conditions of daily use.
Watching the first full billing cycle after installation usually makes the pattern concrete. When energy use rises without a matching gain in output, or when service calls become a recurring line item, the installation has effectively announced its true cost structure. The most useful response is to track these signals early, compare them against the original estimates, and treat the first few months as a live audit rather than a closed deal.
FAQ
Go beyond the spec sheet. Ask about their experience with your product category, including viscosity, particulate size, and foaming behavior. Request line-speed trials with your own containers and closures. A capable exporter will also walk you through local voltage differences, spare parts lead times, and who handles installation and training.
They quietly shape the build. Machines headed to certain regions may need stainless steel grades that meet specific food-contact rules, different safety guarding, or documentation for customs clearance. A seasoned exporter flags these before you order, instead of discovering them at the port.
That depends on how unusual your packaging format is. If your bottle neck, cap style, and fill volume are common, a proven standard model usually runs sooner and costs less to maintain. Customization makes sense when changeover time, headspace requirements, or clean-in-place demands would otherwise force you to compromise daily output.
Expect two maintenance tracks: routine items you can handle in-house, like seal bar cleaning, filter changes, and lubrication, and less frequent work that needs a technician. Good exporters provide a clear schedule, video-guided procedures, and a realistic list of wear parts to keep on the shelf. Ask for that list before the machine ships.
Request a timed demonstration using your actual product and packaging, not a thin water-like substitute. Watch what happens during a minor jam or a short pause: real throughput lives in recovery time and changeover. Also ask for the speed rating at the fill accuracy you require, because running faster often widens fill tolerance.
Ask who answers a technical call on a Friday evening your time, where spare parts are stocked, and how remote diagnostics work. Listen for specifics: a named support contact, average response windows, and whether they can courier critical parts within 48 hours. Vague promises usually mean slow help later.
Yes. Lightweight containers, recyclable films, and shorter production runs are pushing exporters toward gentler handling, quick-change sealing tools, and controls that store recipes digitally. Machines that once favored long runs are being redesigned to stay accurate across more frequent format switches.
Freight, import duties, installation, operator training, and the cost of downtime during commissioning all belong in the comparison. Also consider component availability: a slightly higher machine price can be cheaper over five years if standard parts are easy to source and service calls are rare.
Conclusion
Most buyers spend far too little time asking how an exporter will behave after the machine leaves the factory. The questions that matter are rarely about the brochure: whether the supplier can provide remote troubleshooting in your time zone, who stocks genuine wear parts locally, and how training actually gets delivered when the operators on your floor change shifts. Fill accuracy claims deserve the same scrutiny. A figure measured with water at room temperature says little about hot sauce, foaming detergent, or a viscous cream that settles overnight. Sealing methods add another layer: induction, heat, and ultrasonic options influence not only leak rates but also cap compatibility, residue buildup, energy draw, and how quickly the line can switch to a new container.
Lead times vary for reasons that often have nothing to do with factory floor space. Some exporters keep frames and long-lead items like PLCs, sensors, and sealing heads in stock, while others start procurement only after a deposit clears. The stated machine speed can be equally misleading: a short burst on a test bench is not the same as running three shifts with inconsistent bottle feeding, manual changeovers, and occasional jams. After installation, the quieter costs start appearing, including compressed air consumption, sealing head replacement intervals, travel expenses for service visits, and software updates that are treated as paid extras. Put those next to the initial quote and the smarter packaging decision becomes clear.
Contact Us
Contact Person: Tyson
Email: [email protected]
Tel/WhatsApp: +8613396971296
Website: https://www.wanyingmachinery.com